Ask An Expert
Frequently Asked Questions
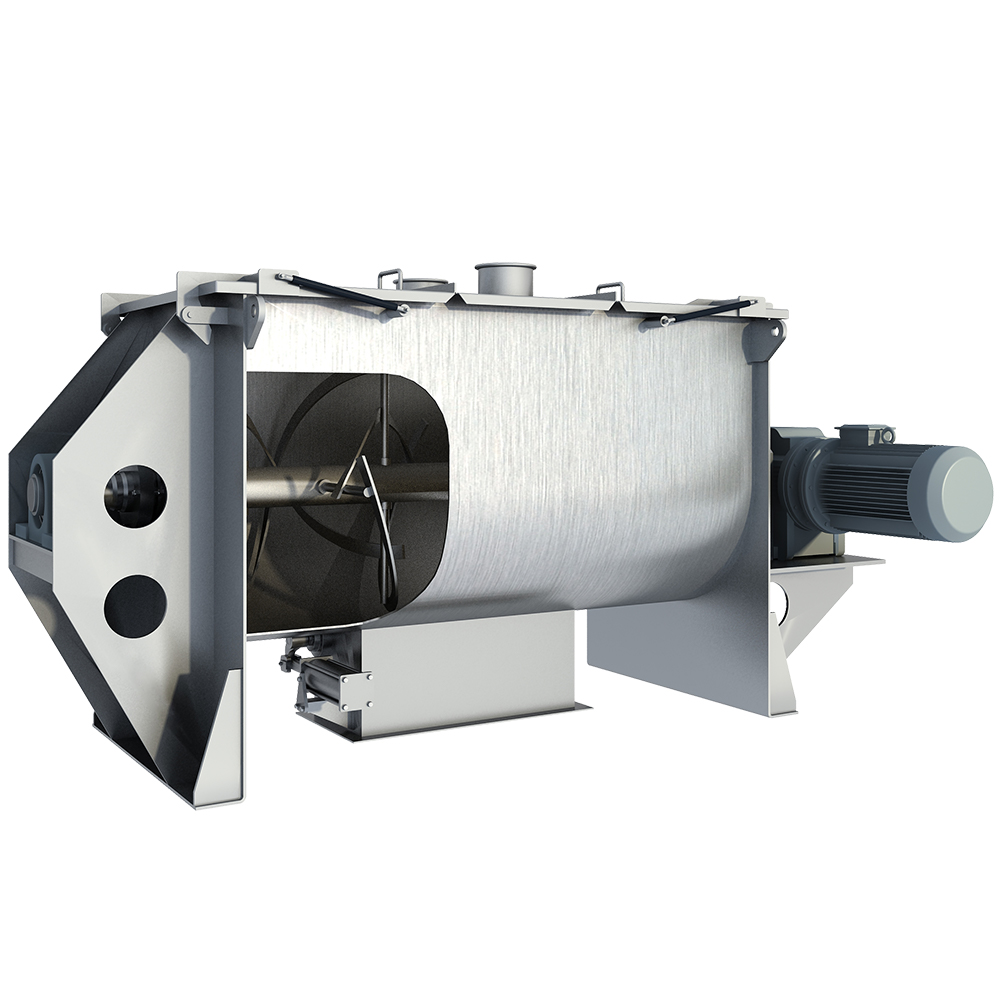
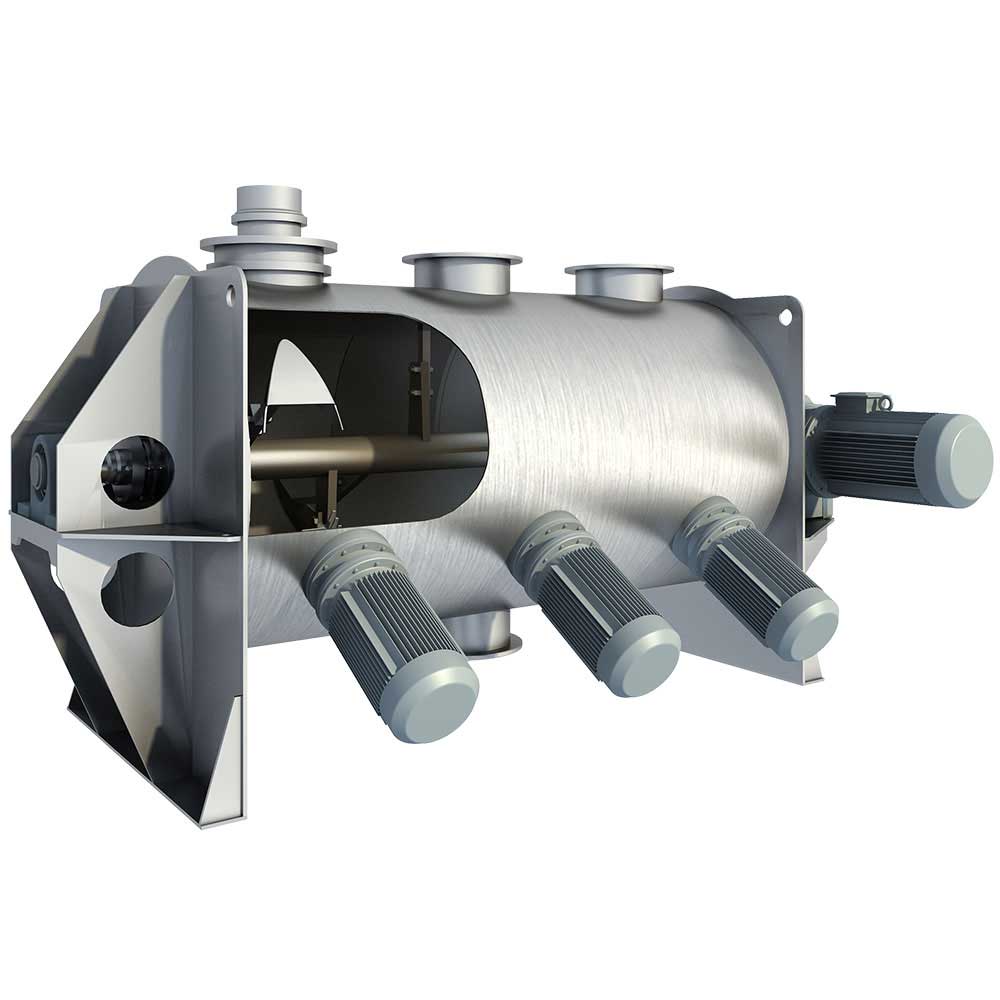
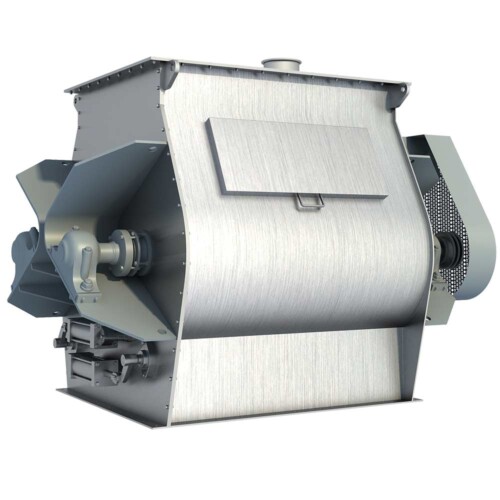
A Ploughshare Mixer is often suitable for materials that tend to agglomerate.
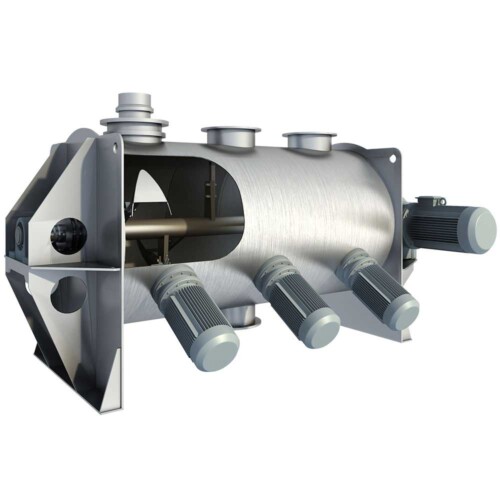
Its plough-shaped mixing tools generate intensive circulation of the material, while optional high-speed choppers can break up lumps and agglomerates during mixing.
The final selection should be based on the material characteristics and process requirements.
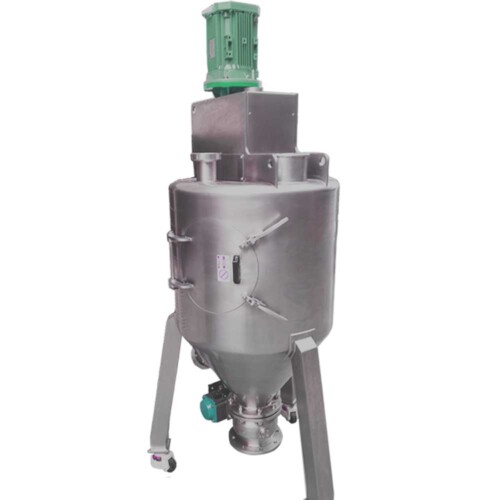
Vortex mixers are designed for a wide variety of powders, granules, and powder-liquid mixtures.
Typical applications include chemical powders, food ingredients, pharmaceutical powders, animal feed, dry mortar, ceramics, battery materials, fertilizers, pesticides, minerals, refractory materials, and other bulk solids. The actual mixer configuration should be selected according to the physical and chemical properties of the material.
Vortex manufacture a wide range of industrial powder and bulk solids mixing equipment, including:
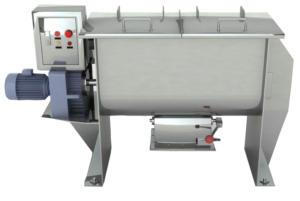
- Horizontal Ribbon Mixers
- Ploughshare Mixers
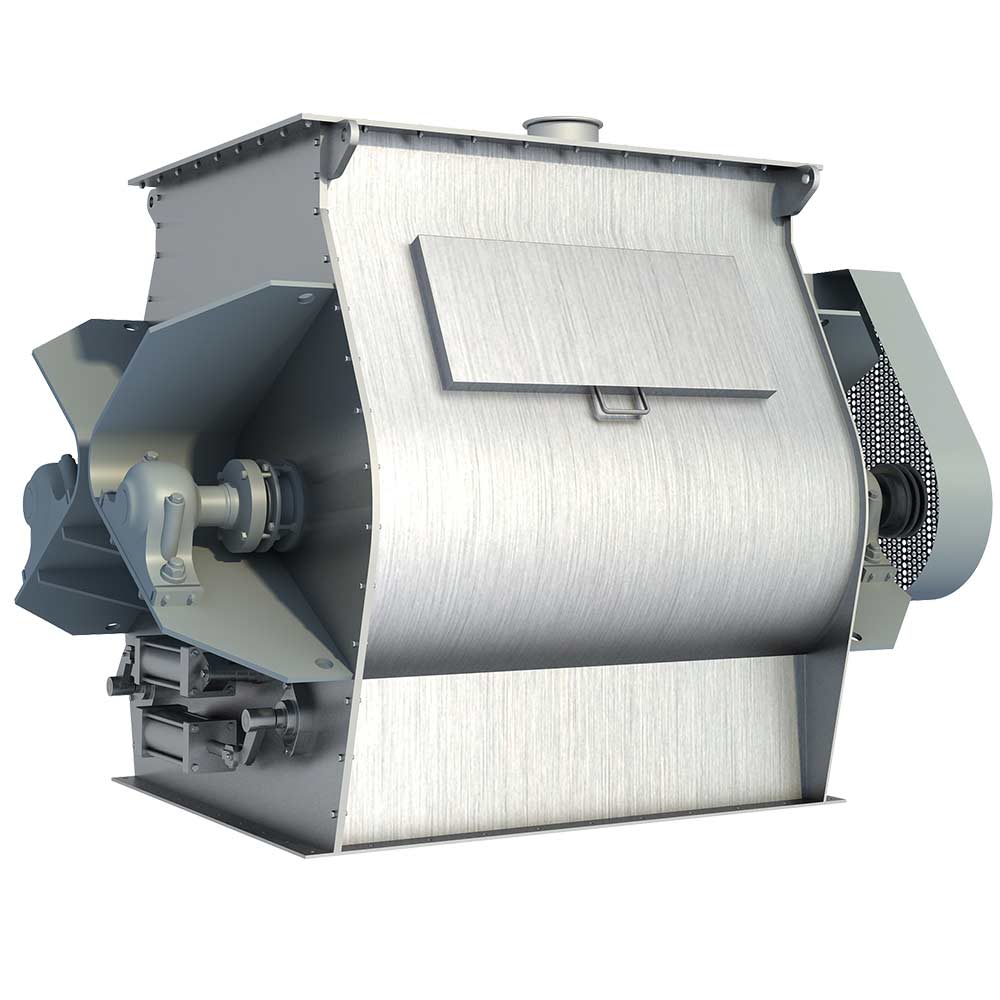
- Double Shaft Paddle Mixers (Paddle Mixers / “No-Gravity” Mixers)
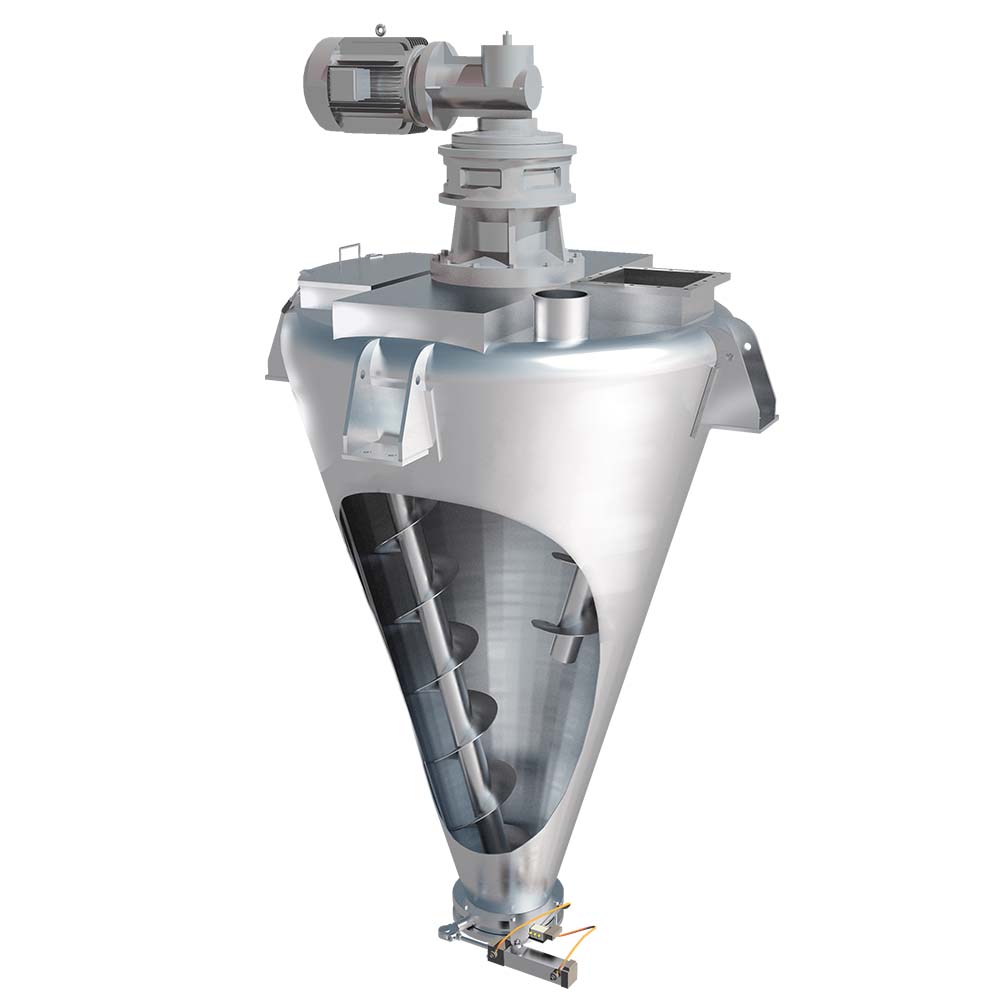
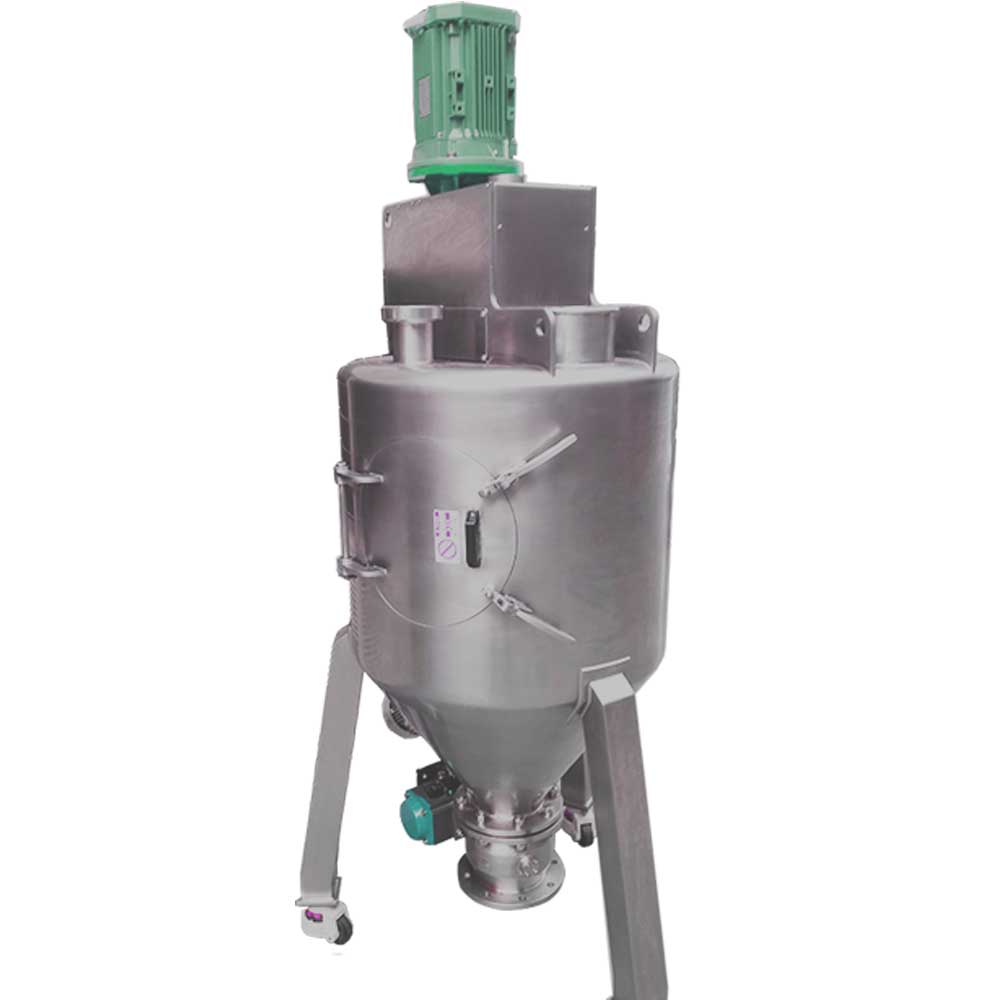
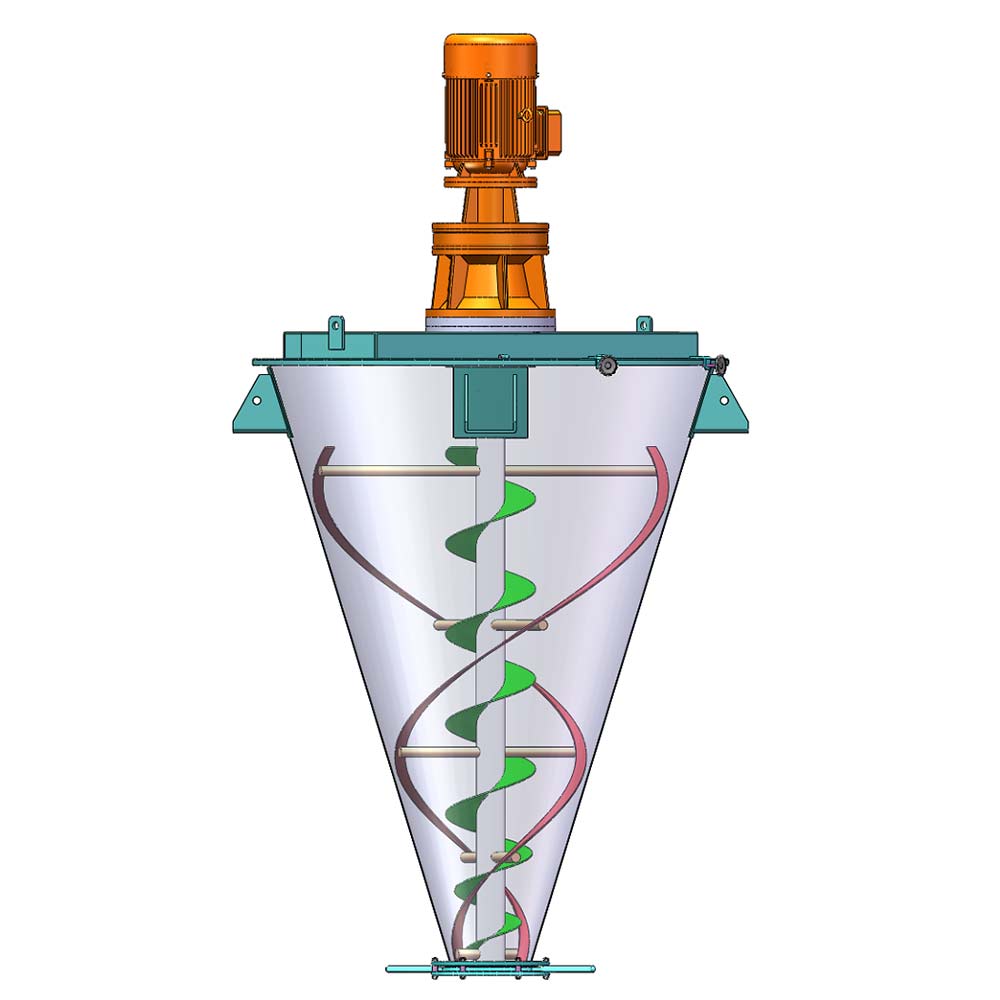
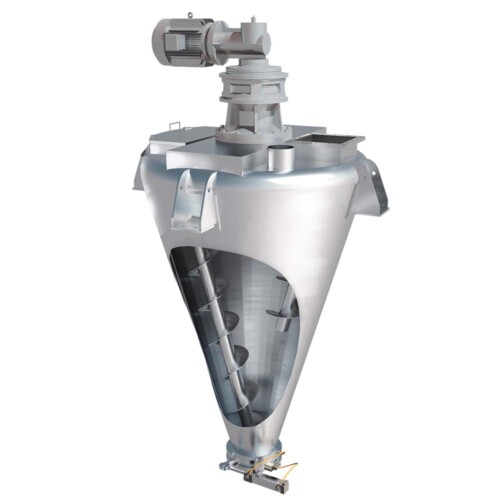
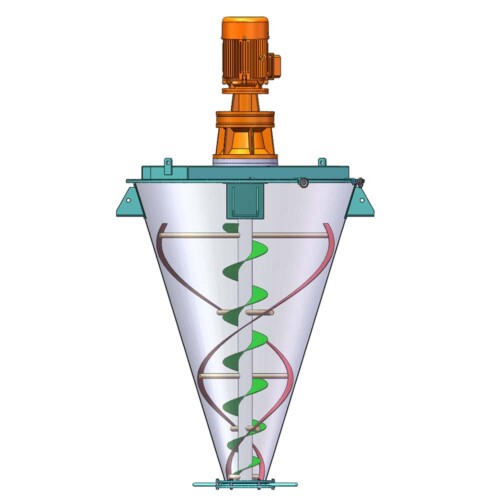
- Conical Twin-Screw Mixers
- Vertical Screw Ribbon Mixers
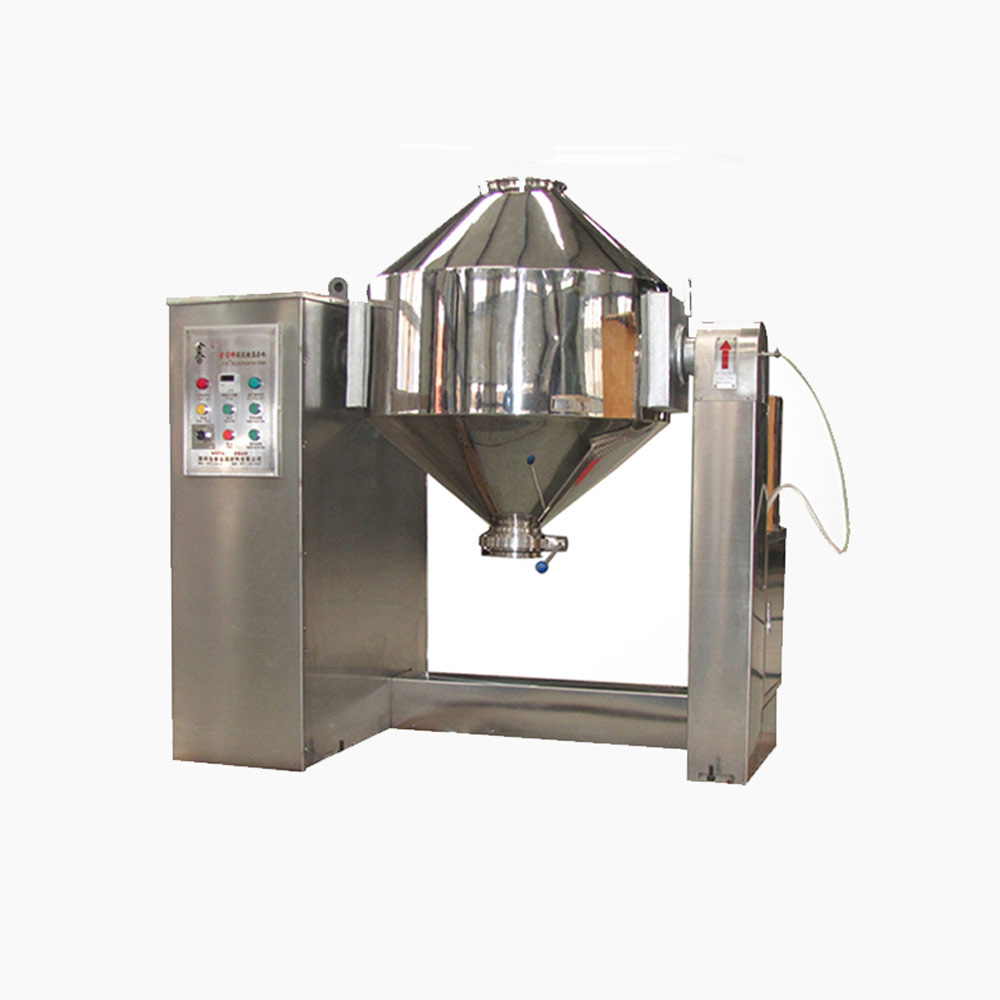
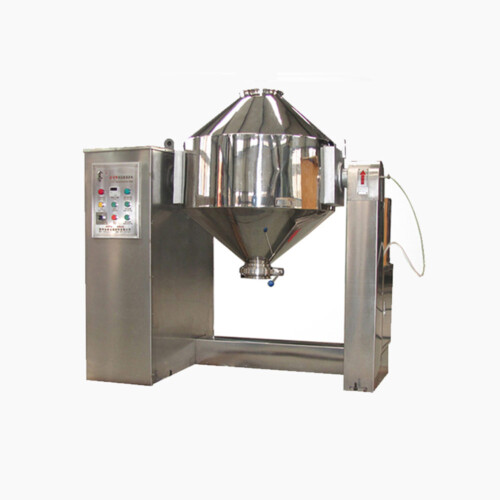
- Double Cone Mixers
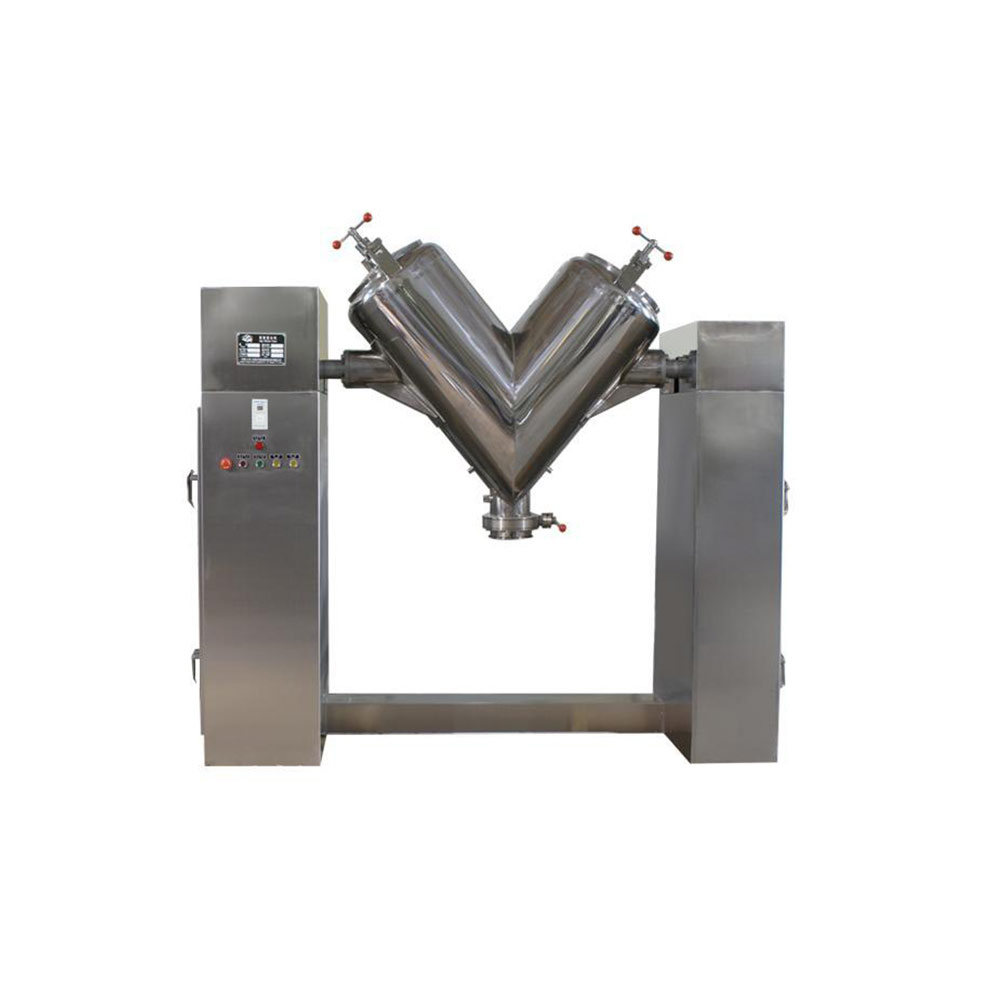
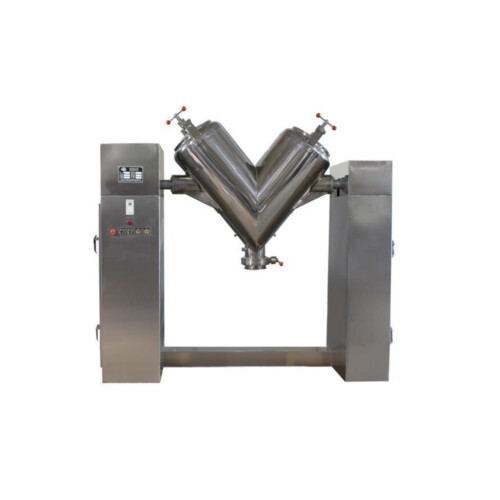
- V-Type Mixers
- 3D Motion Mixers
- Customized mixing systems and complete mixing lines
The most suitable mixer depends on your materials, production capacity, mixing ratio, required mixing time, and process conditions.
Mixer capacity should be evaluated using both the total vessel volume and the effective working volume. The required volume depends on material bulk density, batch weight, filling ratio and the mixing principle of the selected machine. A mixer should not normally be filled to its total geometric volume because sufficient space is required for material movement and effective mixing. For this reason, selecting a mixer based only on vessel volume can result in an unsuitable configuration.
The appropriate industrial powder mixer depends on several factors, including:
- Material characteristics
- Bulk density
- Particle size
- Required mixing uniformity
- Batch size or production capacity
- Moisture content
- Whether heating or drying is required
- Whether liquid addition is required
- Required discharge configuration
- Production and automation requirements
Vortex provides different powder mixer designs so that equipment can be selected according to the specific process requirements.
Vortex powder mixer selection depends on several factors, including:
- Material type and characteristics
- Bulk density and particle size
- Material flowability
- Moisture content
- Viscosity
- Mixing ratio
- Batch size or required production capacity
- Whether liquid addition is required
- Required mixing uniformity
- Temperature, pressure, vacuum, or other process requirements
Vortex engineers can recommend a suitable powder mixer based on your material and process requirements.
Yes, We can supply simple stand alone panels or automated PLC controlled systems. We normally install and test all controls on our mixers before they are shipped.
Yes, we normally test the mixers before they are shipped and mark out the wire need to connect on the control box.
We manufacture specialty mixing equipment for powder & bulk materials. Included are ribbon blender, plough mixer, conical screw mixer, twin shaft paddle mixer, V blender, double cone blender and other auxiliary equipment such as screw conveyor, quantitive auger filler.
We sell across the world, our cusotmers distribute 5 continents.
Share Us With Your Network
Ribbon Blender Mixer: Efficient Powder Mixing for Industrial Applications

Introduction: Why the Used Ribbon Mixers Are Demanded
Industrial mixing is synonymous with various industries such as food manufacturing all the way to pharmaceuticals and chemicals. Companies have a decision to make between the purchase of the newest equipment or the search of other economical options. In this regard, used ribbon mixers are employed. Ribbon mixer/ribbon blender is used to homogeneously mix powders, granules, and semi-wet materials. Acquisition of a used one is not only cost effective, but it also provides efficiency especially in terms of operations.
What is Ribbon Mixer?
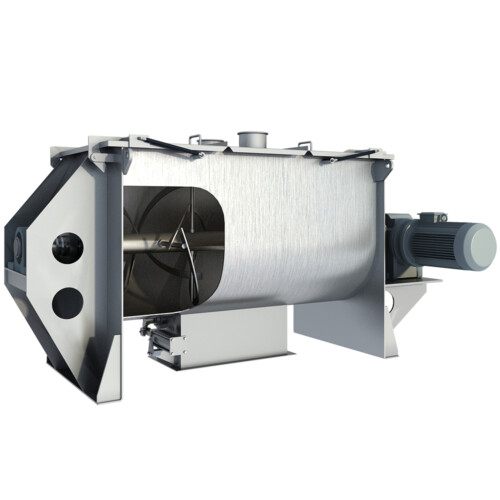
Ribbon mixer this is a form of horizontal mixing equipment fitted with interior and exterior helical ribbons. These ribbons rotate in a U shaped trough to direct materials against each other so that there is homogenous blending. They find large applications in the following industries:
Spices, flour, coffee, protein powders, food processing.
Pharmaceuticals (health supporting powders, supplements)
Fertilizers, detergents, polymers are used as chemicals.
Building materials (powdered cement, dry mortar)
The technology is basic and robust, portraying one of the dynamic and reliable mixer solutions in the industrial market.
What Are the Advantages of Used Ribbon Mixers As opposed to New Ribbon Mixers?
New mixing equipment may cost a lot thus startups and small/medium-sized enterprises may not afford them. The decision to use used ribbon mixers has several benefits:
1. Quality without Cost Increase
A used equipment is normally 40 to 60 percent less expensive than a new machine. There are a lot of second-hand mixers that will still give great performance through proper maintenance.
2. Proven Reliability
Majority of used ribbon mixers are already tested in production conditions and they are durable and consistent in delivering same results.
3. Faster Availability
Purchasing used mixers will entail not waiting four months as the lead time in their manufacture. They can equally be provided on a first-come, first-served basis and businesses can quickly expand upwards.
4. Eco-Friendly and Sustainability Choice
By buying second-hand equipment, it helps conserve the environment and aid in a circular economy hence environmentally sound.
Important Details to Consider when Selecting Ribbon Mixers-Second Hand
There is no single used equipment. Businesses need to take into consideration the following features before buying:
⦁ Capacity: Make sure that the volume of the mixer is the volume you need.
⦁ Material of Construction: Stainless-steel (food and pharma); corn steel (chemicals).
⦁ System demand: Test the power of the motor and the reliability of the gear.
⦁ Ribbons and Seals: Must be fine to assure good mixing and cleanliness.
⦁ Easy to clean: This is essential to industries working with various products.
⦁ Safety Features: Emergency stop switches, protective covers and dust-proof seals.
Industrial Uses of Used Ribbon Mixers
Food Industry
Secondhand ribbon mixers are a common trend in blending flour mixtures, spices, coffee, bakery ingredients as well as protein supplements to provide a constant flavor and texture.
Pharmaceutical Industry
They are essential to develop herbal supplements, herbal drugs, and nutraceutical products by using the exact proportion of blending in the powders.
Chemical Industry
The ideal applications that use ribbon mixers include: detergents, fertilizers, pigments (proper distribution of active constituents), and plastics.
Building Materials and Workmanship
On dry mortar, cement, and other building materials, used mixers are cheaper and provide unified blending results.
The Tips on How to Buy a Quality Used Ribbon Mixer
Purchasing of used equipment should be considered at length. The following are good practices:
⦁ Buy with an Established Supply Company-Always buy supplier that offer inspection reports and warranties.
⦁ Examine Maintenance Records -Machines that have proper maintenance records are safer to invest in.
⦁ Inspection Prior to Buying – Check on their ribbons, seals, and motors to see that they are working properly.
Demand a Test Run The live demonstration testifies to the reliability of the mixer.
Factor New Ribbon Mixer Used Ribbon Mixer
Price Range High (100% cost) 40–60% lower
Availability 6–12 weeks Immediate
Reliability High High (if well-maintained)
Environmental Impact Higher footprint Eco-friendly
FAQs on Used Ribbon Mixers
Q1: Is food processing safe in used ribbon mixers?
Yes, provided that they are stainless steel models and clean them with hygienic seals and cleaning provisions.
Q2: What is the lifespan of a ribbon mixer?
With good maintenance, a ribbon mixer has a capacity of 10-15 years where it is used intensively.
Q3: are warranty provided with used ribbon mixers?
Credit capable dealers usually give warranty or service guarantees on secondhand equipment.
Q4: Will I be able to scale production using a used mixer?
Yes. Secondhand mixers come in a variety of capacities, small batch or large production.
Conclusion
Used ribbon mixers provide a viable option to companies that desire high-quality mixing devices and do not have the huge budget to spend on buying a new one. These mixers with the right maintenance and sources of sources of materials can give good performance, dependability and value and economy over a long period of time in any industry. Whether you deal with food, pharmaceuticals, chemicals or construction, a used ribbon mixer can be the solution to make you optimize your production lines.
Ask An Expert