Ask An Expert
Frequently Asked Questions
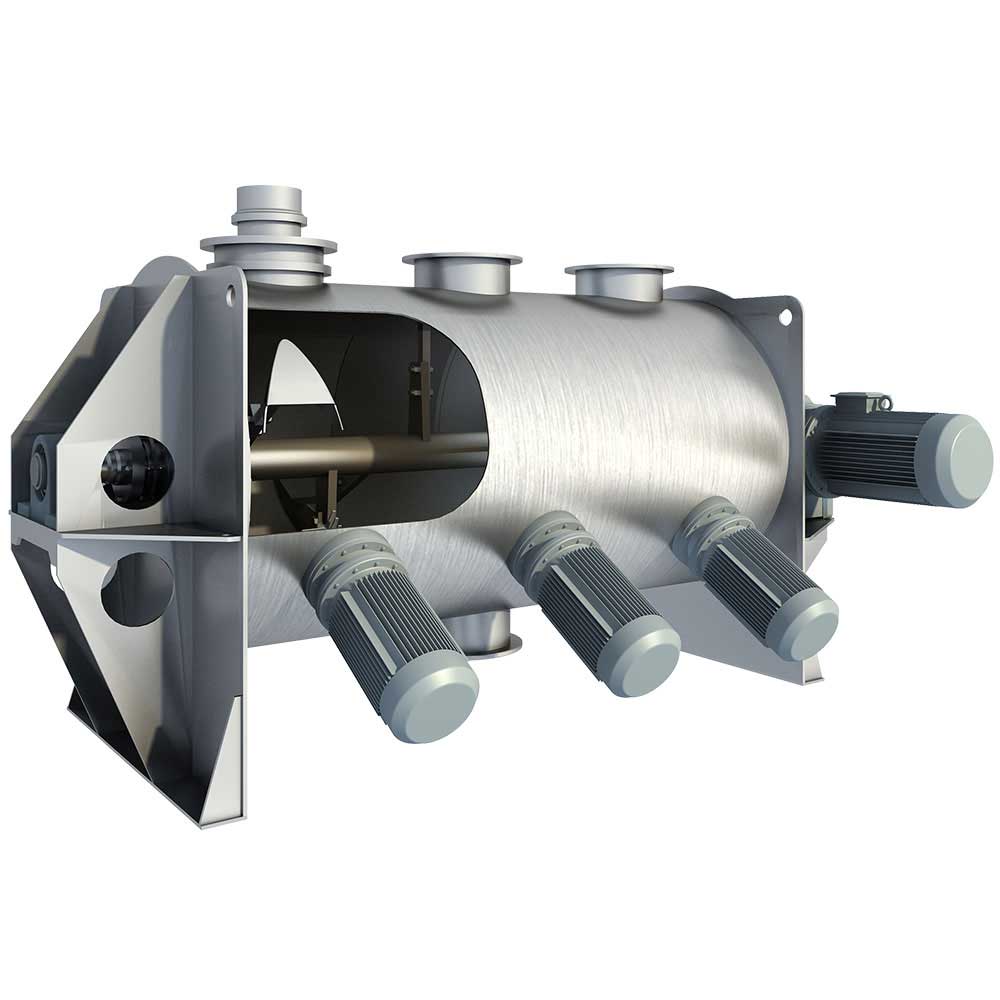
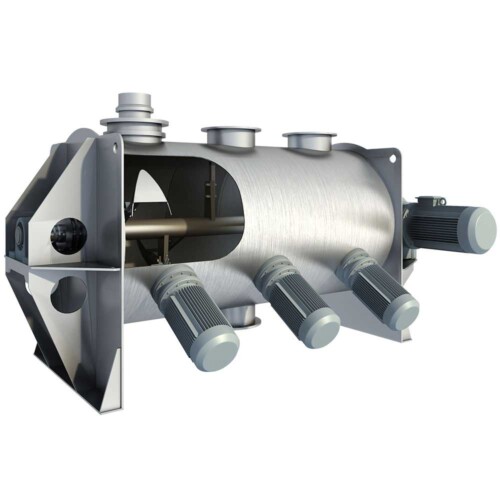
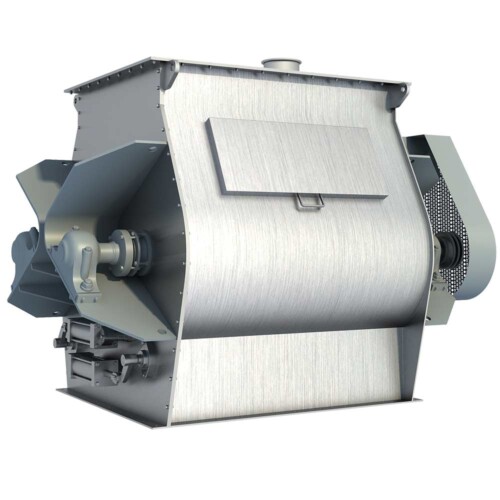
A Ploughshare Mixer is often suitable for materials that tend to agglomerate.
Its plough-shaped mixing tools generate intensive circulation of the material, while optional high-speed choppers can break up lumps and agglomerates during mixing.
The final selection should be based on the material characteristics and process requirements.
Vortex mixers are designed for a wide variety of powders, granules, and powder-liquid mixtures.
Typical applications include chemical powders, food ingredients, pharmaceutical powders, animal feed, dry mortar, ceramics, battery materials, fertilizers, pesticides, minerals, refractory materials, and other bulk solids. The actual mixer configuration should be selected according to the physical and chemical properties of the material.
Vortex manufacture a wide range of industrial powder and bulk solids mixing equipment, including:
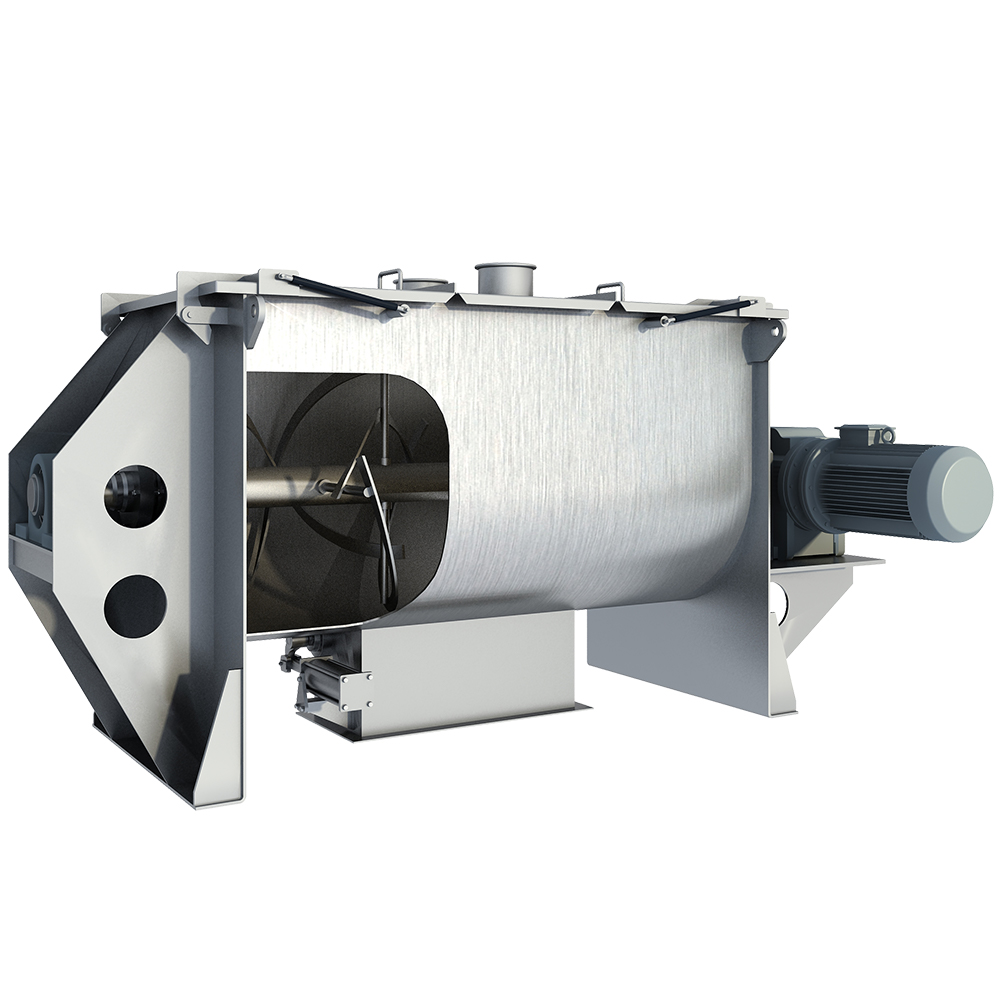
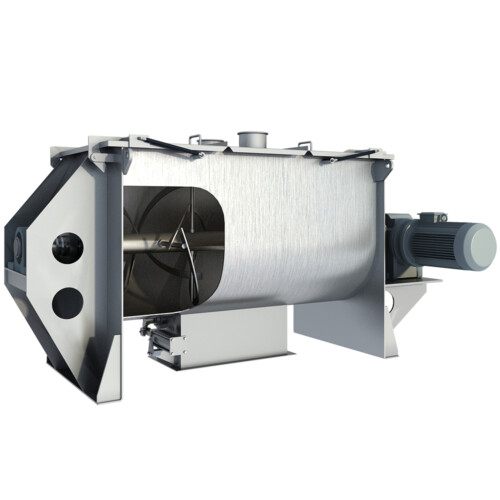
- Horizontal Ribbon Mixers
- Ploughshare Mixers
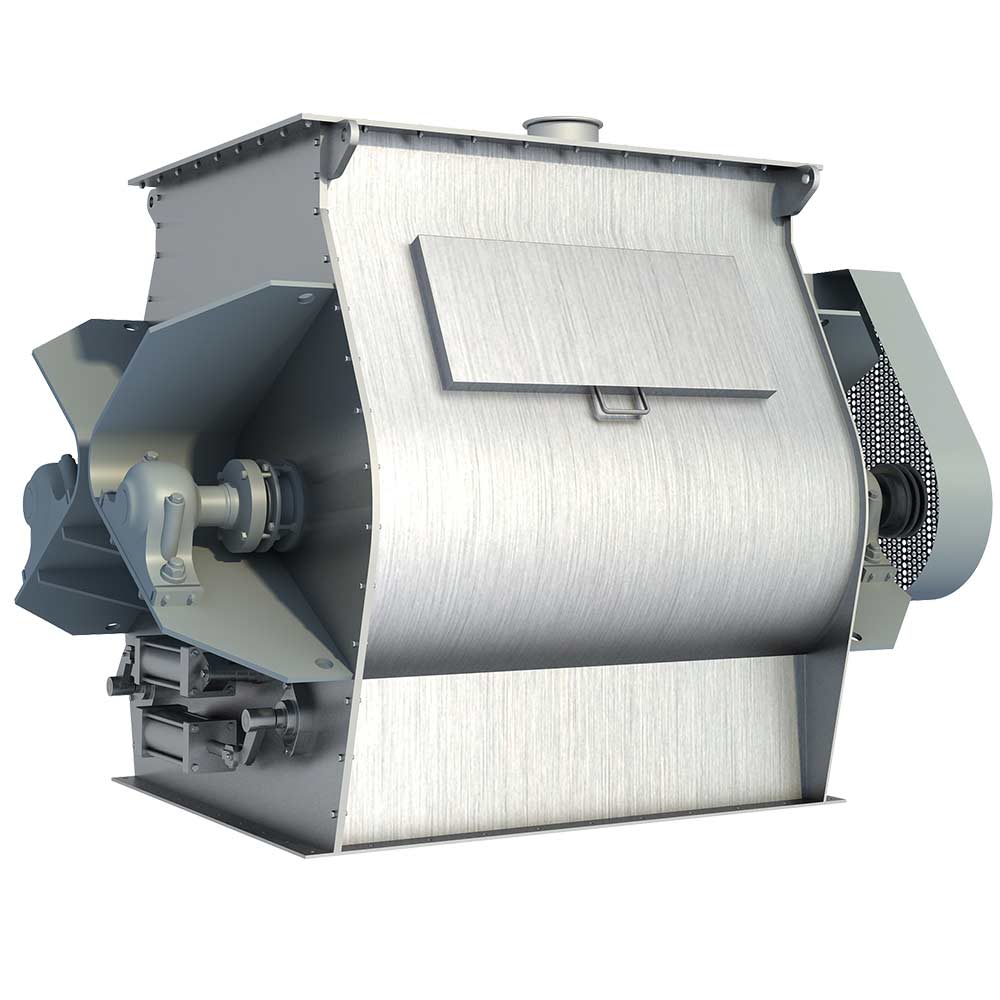
- Double Shaft Paddle Mixers (Paddle Mixers / “No-Gravity” Mixers)
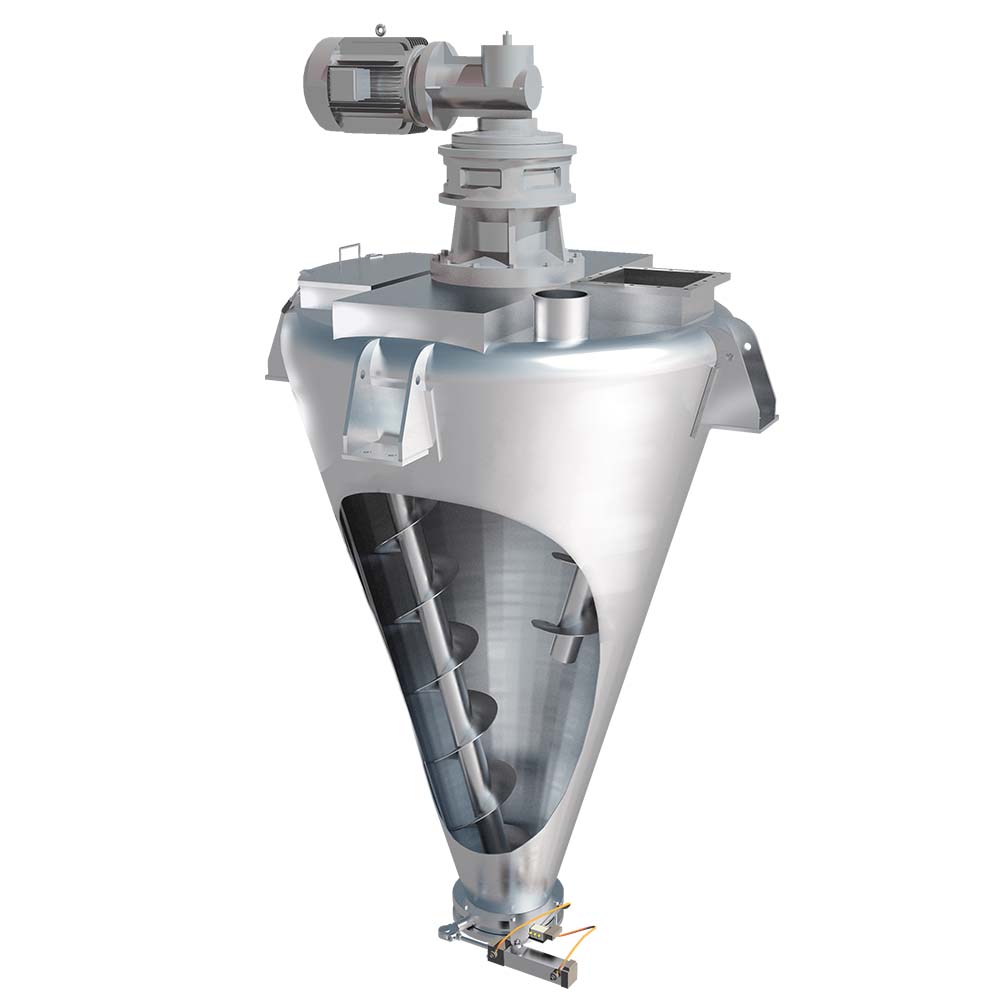
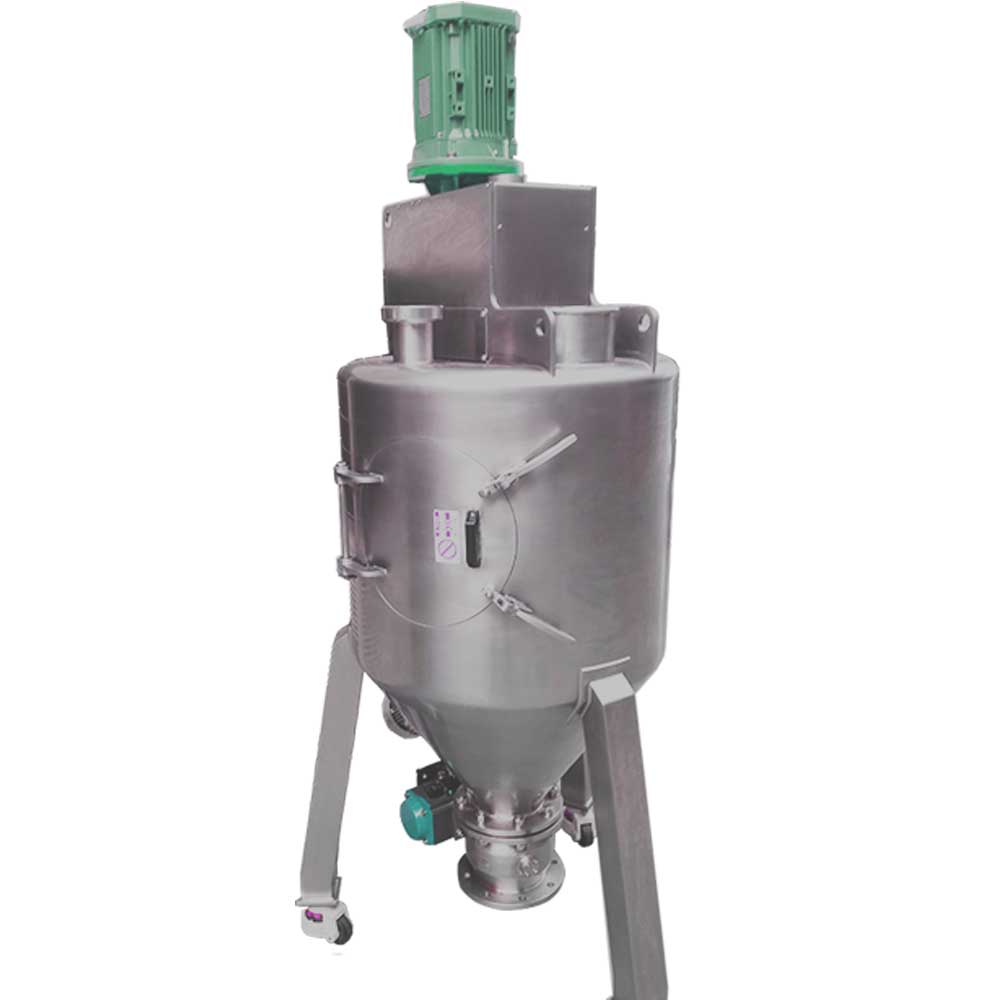
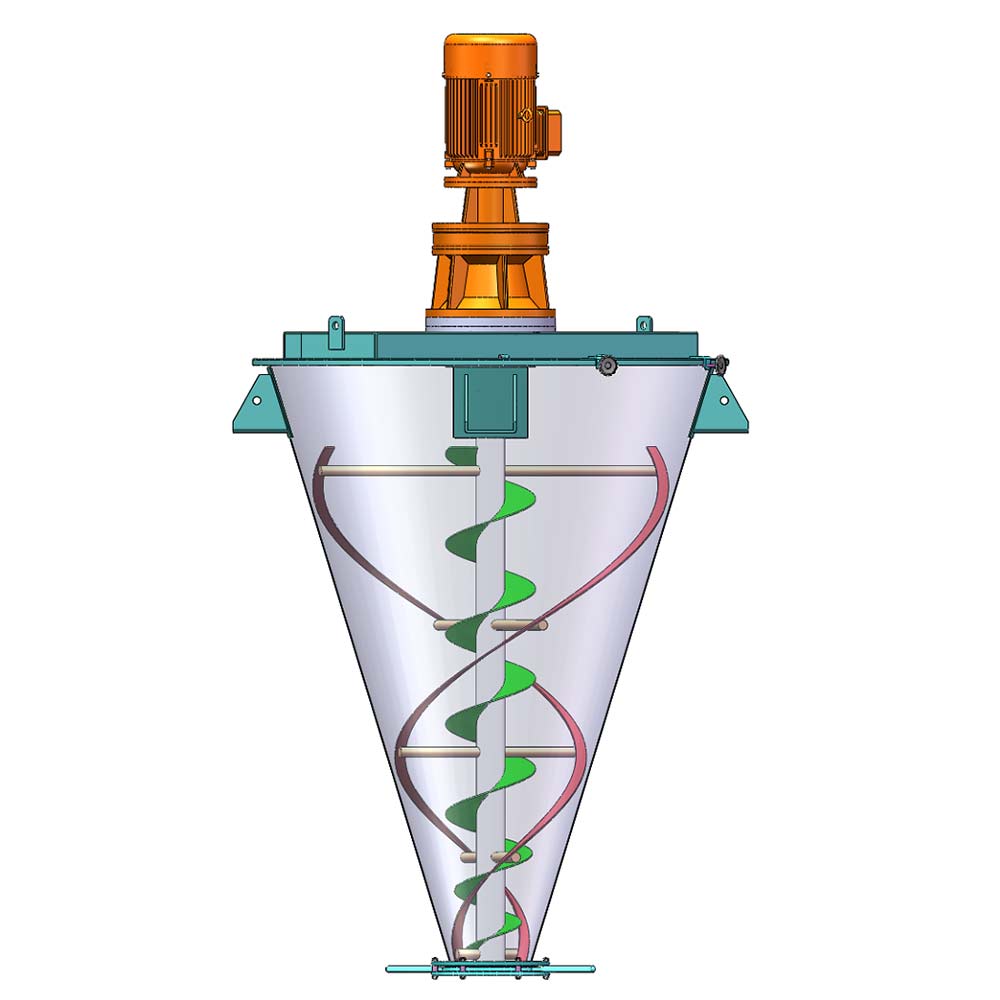
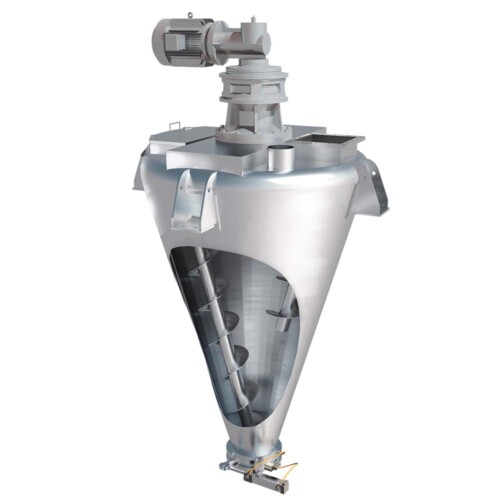
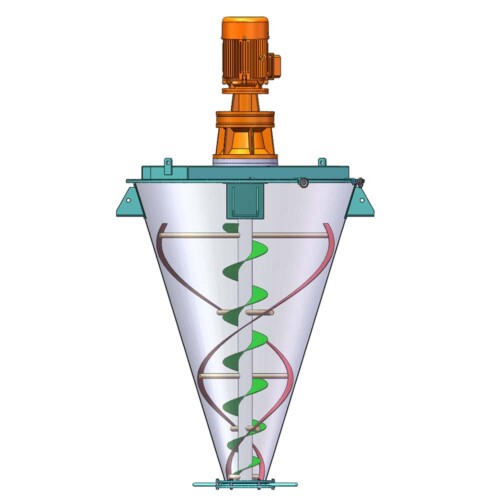
- Conical Twin-Screw Mixers
- Vertical Screw Ribbon Mixers
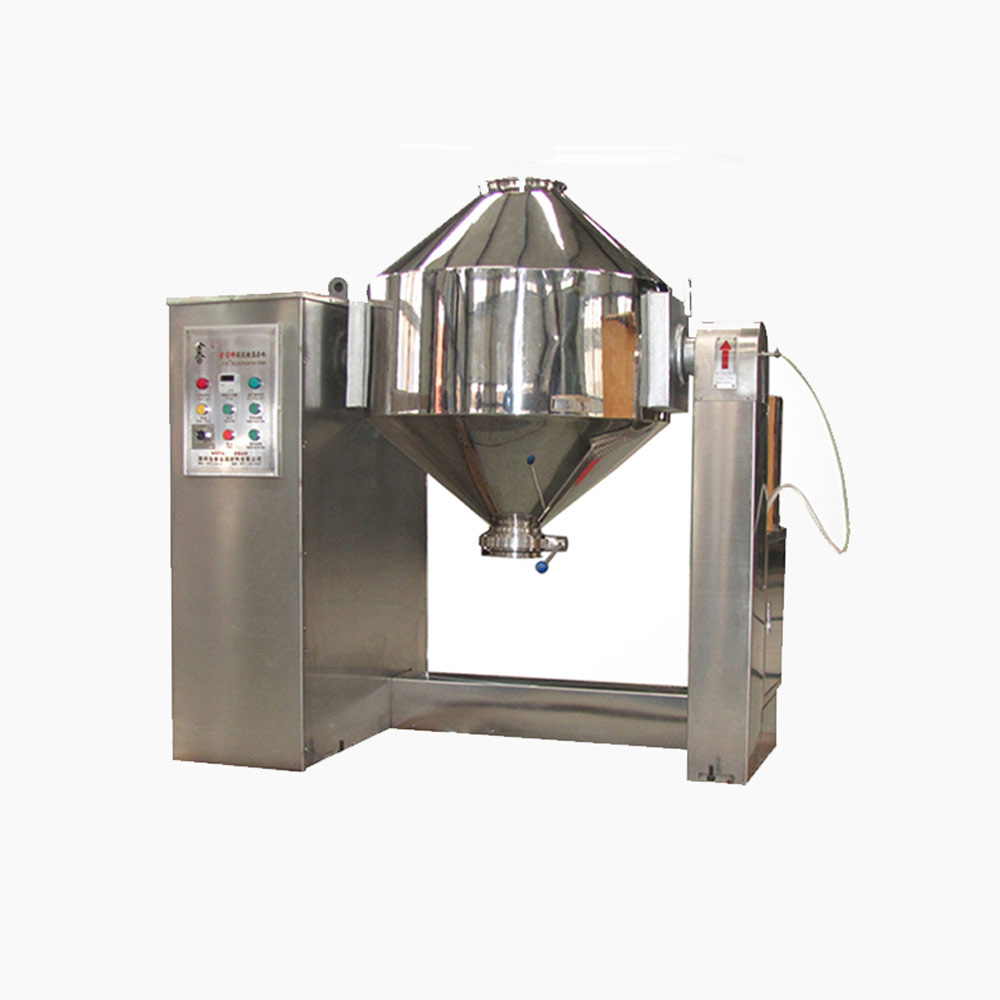
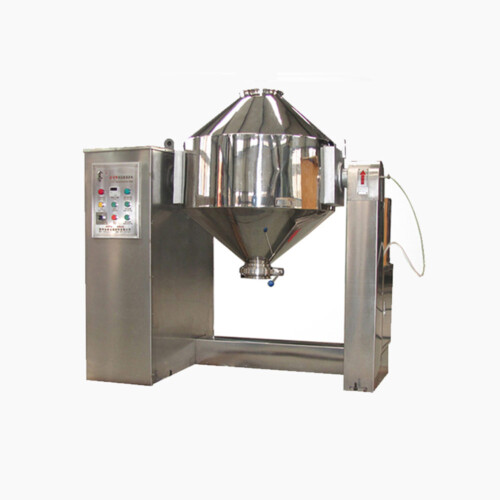
- Double Cone Mixers
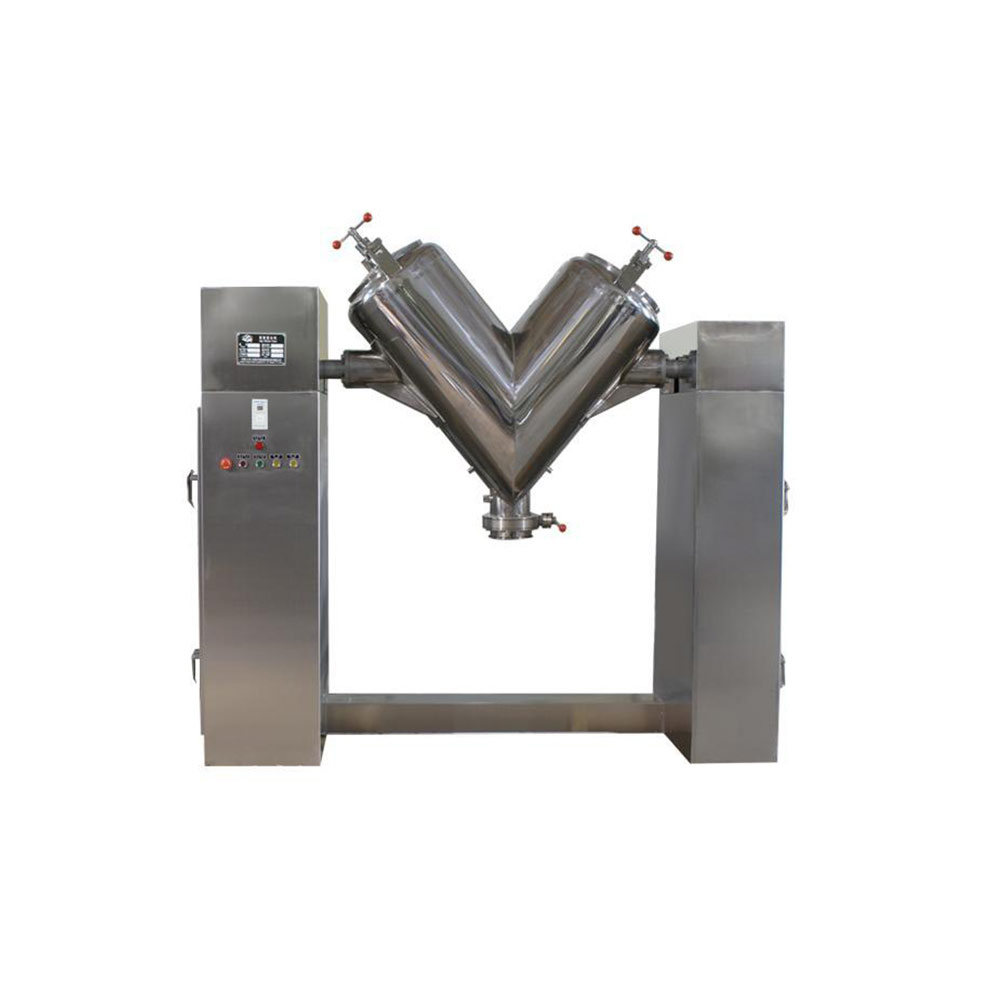
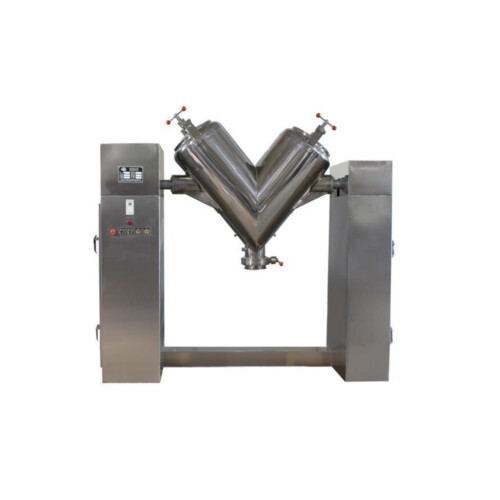
- V-Type Mixers
- 3D Motion Mixers
- Customized mixing systems and complete mixing lines
The most suitable mixer depends on your materials, production capacity, mixing ratio, required mixing time, and process conditions.
Mixer capacity should be evaluated using both the total vessel volume and the effective working volume. The required volume depends on material bulk density, batch weight, filling ratio and the mixing principle of the selected machine. A mixer should not normally be filled to its total geometric volume because sufficient space is required for material movement and effective mixing. For this reason, selecting a mixer based only on vessel volume can result in an unsuitable configuration.
The appropriate industrial powder mixer depends on several factors, including:
- Material characteristics
- Bulk density
- Particle size
- Required mixing uniformity
- Batch size or production capacity
- Moisture content
- Whether heating or drying is required
- Whether liquid addition is required
- Required discharge configuration
- Production and automation requirements
Vortex provides different powder mixer designs so that equipment can be selected according to the specific process requirements.
Vortex powder mixer selection depends on several factors, including:
- Material type and characteristics
- Bulk density and particle size
- Material flowability
- Moisture content
- Viscosity
- Mixing ratio
- Batch size or required production capacity
- Whether liquid addition is required
- Required mixing uniformity
- Temperature, pressure, vacuum, or other process requirements
Vortex engineers can recommend a suitable powder mixer based on your material and process requirements.
Yes, We can supply simple stand alone panels or automated PLC controlled systems. We normally install and test all controls on our mixers before they are shipped.
Yes, we normally test the mixers before they are shipped and mark out the wire need to connect on the control box.
We manufacture specialty mixing equipment for powder & bulk materials. Included are ribbon blender, plough mixer, conical screw mixer, twin shaft paddle mixer, V blender, double cone blender and other auxiliary equipment such as screw conveyor, quantitive auger filler.
We sell across the world, our cusotmers distribute 5 continents.
Share Us With Your Network
Bulk and Tapped Density of Mixture
Introduction to Bulk and Tapped Density
The bulk density of a material is the ratio of the mass to the volume (including the interparticulate void volume) of an untapped powder sample.
The tapped density is obtained by mechanically tapping a graduated cylinder containing the sample until little further volume change is observed.
Instrument and measuring principle
The bulk density is given in g/ml. The bulk density depends on both the density of the powder particles and on the arrangement of the powder particles. The bulk density is influenced by the preparation, treatment and storage of the sample material. A method for measuring the bulk and tapped density of powders is described in the European Pharmacopoeia chapter 2.9.34.
More about the methods
Bulk method 1: The bulk density is obtained by adding a known mass of powder to a graduated cylinder. The density is calculated as mass/volume.
Tapped method 1:The tapped density is obtained by mechanically tapping a graduated cylinder containing the sample until little further volume change is observed. The tapping can be performed using different methods. The tapped density is calculated as mass divided by the final volume of the powder. The interparticulate interactions that influence the bulking properties of a powder are also the interactions that interfere with powder flow. It is therefore possible to gain information about the relative importance of these interactions in a given powder by comparing the bulk and tapped densities, and such a comparison can be used to index the ability of the powder to flow.
The compressibility index and Hausner ratio are measures of the products ability to settle, and permit an assessment of the relative importance of interparticulate interactions. In a free-flowing powder these interactions are less significant and the bulk and tapped densities will be closer in value. For poorly flowing materials, there are greater interparticulate interactions and a greater difference between the bulk and tapped densities will be observed. The differences are reflected in the compressibility index and Hausner ratio.
Compressibility index:

Hausner ratio:

V0 = unsettled apparent volume (bulk volume) Vf = final tapped volume
As seen in the table below the copresibility index and Haussner ratios can be used to estimate the flow characteristics of the powder.
| Compressibility index (per cent) | Flow character | Hausner ratio |
| 1-10 | Excellent | 1.00-1.11 |
| 11-15 | Good | 1.12-1.18 |
| 16-20 | Fair | 1.19-1.25 |
| 21-25 | Passable | 1.26-1.34 |
| 26-31 | Poor | 1.35-1.45 |
| 32-37 | Very poor | 1.46-1.59 |
| > 38 | Very, very poor | > 1.60 |
| (1) Carr RL. Evaluating flow properties of solids. Chem Eng 1965; 72:163-168. | ||
Ask An Expert